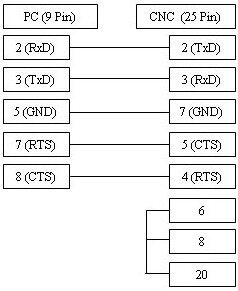
Establishing reliable RS232 serial communication between your PC and the Amada CNC control is fundamental for successful DNC operations. Ensure that communication parameters—specifically baud rate, parity, and data bits—are matched precisely between the software and the controller settings. Using ISO code is standard practice for Amada systems to minimize character interpretation errors. If you experience data transmission stalls or buffer overflows, verify your cable configuration; ensure it is properly wired for either software (XON/XOFF) or hardware (RTS/CTS) handshaking. Mismatched flow control is the most common cause of communication failure. Always verify your cable shielding and length to prevent electrical noise interference in the shop floor environment, which can corrupt data packets during high-speed DNC streaming.
| Parameter |
Value |
Comments |
| Baud Rate | 2400 | |
| Parity | Even | |
| Databits | 7 | |
| Stop Bits | 2 | |
| Punch Code | 1 | 0=EIA 1=ISO (ISO recommended) |
| Dec Inp | 0 | |
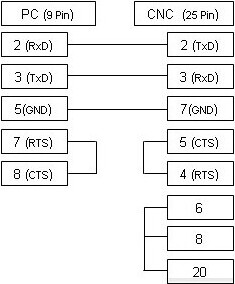
The cable illustrated above is the most frequently used configuration, supporting xOn/xOff (DC1/DC3) flow control. If your CNC machine is specifically configured for RTS/CTS (hardware) handshaking, please refer to the alternative wiring diagram below, which typically accommodates both methods of flow control.