Bridgeport Boss CNC controls are renowned for their rugged reliability on the shop floor; however, they demand precise serial port configuration to ensure seamless DNC communication. Establishing stable data transfer requires strict adherence to baud rate, parity, and data bit synchronization. Users frequently encounter parity errors or buffer overflows due to handshaking mismatches—specifically when conflicting with software (XON/XOFF) or hardware (RTS/CTS) flow control protocols. By utilizing the dedicated DNC Port B and matching your PC’s COM settings to the controller’s legacy requirements, you can eliminate intermittent transmission drops. Always verify your cable shielding and pin-out configurations to prevent signal interference, which is the most common cause of checksum errors during prolonged machining cycles.
| Parameter |
Value |
Comments |
| Baud Rate |
4800 |
|
| Parity |
Even |
|
| Databits |
7 |
|
| Stop Bits |
1 |
| Use DNC Port B |
| In EasyDNC set Baud Rate, Parity, DataBits and StopBits as above. Set 'Mode=Auto' |
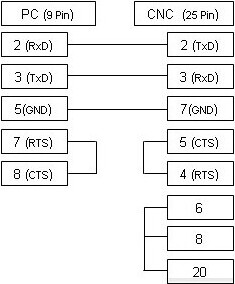
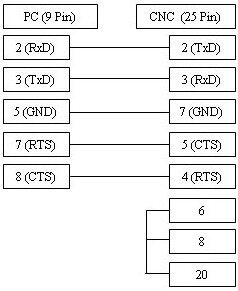
The cable diagram shown above is the most frequently used configuration and supports XON/XOFF (DC1/DC3) flow control. If your CNC machine is specifically configured for hardware-based RTS/CTS flow control, please refer to the alternative wiring diagram below, which is designed to support both methods of flow control in most operational environments.