The Hinumerik 2000M and 2000T controls require precise RS232 interface parameter configuration to ensure stable, reliable data transmission during DNC operations. By accurately setting the baud rates via parameters 5011 and 5013, and correctly implementing RTS/CTS hardware handshaking or XOn/XOff software flow control, you can effectively mitigate common transmission errors such as parity mismatches or buffer overflows. Proper configuration is essential for seamless CNC program transfers, especially when handling large, complex files. If communication timeouts occur, verify that your data cable wiring matches the control's DTE/DCE requirements and ensure that stop bit and flow control settings are mirrored exactly between the control and your DNC software to prevent intermittent data corruption or machine-side communication alarms.
| Parameter | Value | Comments |
|---|---|---|
| 5010 | 0 | (00000000) |
| 5012 | 0 | (00000000) |
| 5011 | 11000101 | = 2400 Baud. See table below for others |
| 5013 | 11000101 | = 2400 Baud. See table below for others |
| 11000011 = 600 | 11000100 = 1200 | 11000101 = 2400 | 11000110 = 4800 | ||
| 5016 | xx10xxxx | x = Leave unchanged |
| RTS | Line 1 | Select RTS/CTS in DNC software |
Cable Wiring and Notes
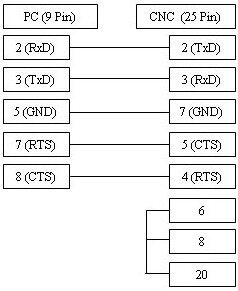
The cable shown here works with XOn/XOff (DC1/DC3) flow control as well as RTS/CTS hardware flow control. If your CNC does not require flow control, a simple 3-wire cable can be used (Diagram here).
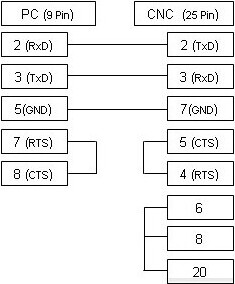
RS232 Cable: 9-pin (PC) to 25-pin (CNC)