Establishing reliable RS232 serial communication for the Hinumerik 3100M and 3100T controls requires precise machine parameter configuration. Successful DNC data transfer relies on matching baud rates, handshake protocols, and cabling specifications between your PC and the CNC. Effective troubleshooting involves ensuring the parity, stop bits, and flow control (RTS/CTS vs. XON/XOFF) are synchronized to prevent buffer overflows or framing errors during transmission. Our configuration guide assists you in correctly setting parameters 411, 412, and 416, ensuring seamless data exchange and robust DNC operations. Always verify that your communication cable shielding is properly grounded at the PC end to mitigate electrical noise, which remains a frequent cause of intermittent transmission failures in industrial environments.
| Parameter | Value | Comments |
|---|---|---|
| 411 | 1110 1101 | = 2400 Baud. See table below for other baud rates |
| 412 | 1110 1101 | = 2400 Baud. See table below for other baud rates |
|
1110 1011 = 600 Baud 1110 1100 = 1200 Baud 1110 1101 = 2400 Baud 1110 1110 = 4800 Baud |
||
| 416 | 1xxxxxx1 | x = Leave unchanged |
| Select RTS/CTS flow control in your DNC software. | ||
Cable Wiring and Notes
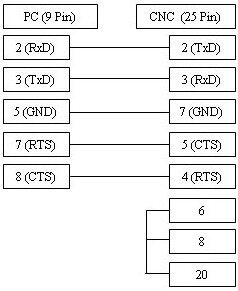
The cable diagram provided here supports both XOn/XOff (DC1/DC3) flow control and RTS/CTS (hardware flow control), ensuring compatibility in most industrial applications.
However, if you are certain your CNC does not utilize hardware flow control—or strictly requires XOn/XOff only—you may utilize a simpler 3-wire cable configuration. A diagram for this can be found here.
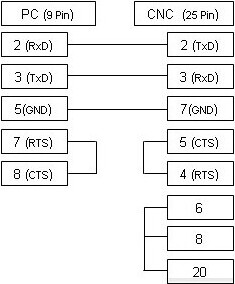
RS232 Cable (9-pin PC to 25-pin CNC):