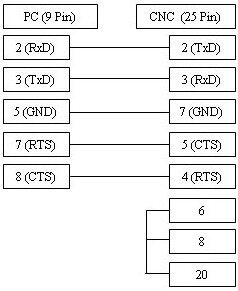
Configuring the Fanuc Oi controller requires precise machine parameter settings and a verified physical interface connection. Establishing stable DNC (drip-feed) communication demands that baud rate, stop bits, and flow control (software XON/XOFF or hardware RTS/CTS) match exactly between the EasyDNC software and the Fanuc control. Common connection pitfalls include mismatched parity settings or handshake protocol conflicts. When troubleshooting, ensure the I/O channel aligns with your physical port assignment and verify that cabling follows standard RS-232 pinout specifications to avoid buffer overflows or frame errors during high-speed data transmission. Use the following parameters as a baseline to ensure reliable, high-performance serial communication between your PC and your CNC machine.
| Parameter |
Value |
Comments |
| 0000 | 00000010 |
| 0020 | 0 |
| 0100 | 00100000 |
| 0101 | 10000001 |
| 0102 | 0 |
| 0103 | 9 (BaudRate 2400) |
| | 6 = 300 / 7 = 600 / 8 = 1200 / 9 = 2400 / 10 = 4800 / 11 = 9600 |
| TV Check | 0 = Disabled |
| Punch Code | 1 = ISO |
| I/O Channel | 0 |
| Drip Feed: Select Auto/DNC mode on the control. Press Cycle Start. Then go to the computer, prepare the program and click 'Send'. As data begins to flow the machine moves. |
| In EasyDNC set Baud Rate, Parity, DataBits and StopBits as above. Set 'Mode=Auto or Fanuc'. |
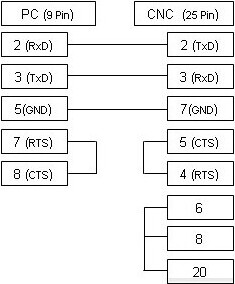
The cable illustrated above is the most commonly used version and supports XON/XOFF (DC1/DC3) flow control. If your CNC machine is configured for RTS/CTS (hardware) flow control, please refer to the alternative wiring diagram below, which typically supports both methods of communication.