The Yasnac LX and MX series are highly regarded for their robust, production-grade performance. Establishing stable RS232 serial communication is critical for reliable DNC operation. Ensure that these parameters are accurately mirrored within the machine controller to prevent buffer overflows or data parity errors during program transfer. When troubleshooting connectivity, verify that your baud rate matches precisely between the PC and the CNC. If you experience "Buffer Overflow" alarms, ensure your handshaking protocol—either Software (XON/XOFF) or Hardware (RTS/CTS)—is strictly enforced. For older LX/MX-1 units, prioritize verifying cable shielding and signal ground integrity to mitigate EMI, which often causes intermittent transmission failures in high-vibration manufacturing environments.
| Parameter | Value | Comments |
|---|---|---|
| 6000 | 1xxx xxxx | x = Do not change |
| 6001 | 1xxx xxxx | (Potentially required for MX-2 only) |
| 6003 | xxx1 xxx1 | |
| 6021 | x111 xx1x | (Potentially required for LX/MX-1 only) |
| 6022 | xxxx xx11 | |
| 6026 / 6028 | 0001 1000 | Baud Rate = 2400 |
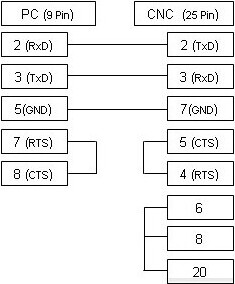
Cable Pinout and Connection Guide
The cable configuration shown here is the most common standard for xOn/xOff (DC1/DC3) flow control. If your CNC machine is specifically configured for RTS/CTS (Hardware Handshake) flow control, please refer to the alternative cable diagram here.
RS232 Cable: 9-pin (Computer) to 25-pin (CNC)