Establishing stable serial DNC communication for Mazak M Plus and T Plus controls requires precise configuration of user parameters, specifically regarding baud rate and handshake protocols. To ensure seamless data transfer between your PC and the machine, accurate adjustment of parameters G1 through G48 is essential. A common pitfall in these legacy systems is the discrepancy between controller settings and software interpretation; notably, even when the Mazak is configured for 8-bit data, the DNC software must often be set to 7 data bits to prevent framing errors or transmission stalls. Always verify cable integrity and ensure your flow control settings (XON/XOFF vs. hardware handshaking) are correctly matched on both ends to avoid buffer overflows during long program transfers.
| Parameter | Value | Comments |
|---|---|---|
| User Parameter #5 | ||
| G1 | 1 | Baud Rate 9600 |
| G2 | 3 | 2 Stop Bits |
| G3 | 0 | Even Parity |
| G5 | 3 | 8 Data Bits (Set DNC software to 7 data bits) |
| G6 | 1 | - |
| G10 | 3 | xOn/xOff Flow Control (DC1 and DC3) |
| G12 | 0 | No DC2 and DC4 |
| G13 | 50 | - |
| G17 | 00000000 | - |
| G31 | 00000000 | - |
| G33 | 50 | - |
| G34 | 10 | - |
| G39 | 00000100 | - |
| G40 | 00000000 | - |
| G48 | 0 | - |
Cable Pinout and Notes
Note: Although the Mazak is set to 8 data bits, ensure your DNC software is set to 7 data bits. Select xOn/xOff flow control within the DNC software settings.
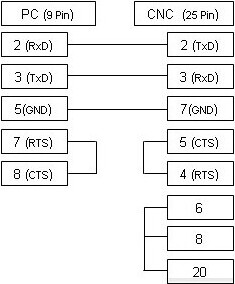
The cable shown above supports xOn/xOff (DC1/DC3) flow control.
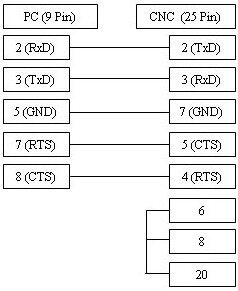
If your machine requires RTS/CTS hardware flow control, use this alternative wiring diagram.