The Fagor 80xx control is a robust and widely utilized system in precision industrial manufacturing. Establishing a reliable DNC link requires strict alignment of RS232 serial parameters between the machine and your PC. Common communication failures often stem from baud rate mismatches or conflicting handshaking protocols. Ensure that your data bits, parity, and stop bits match exactly within EasyDNC. If you experience character drops or buffer overflows, verify that your XON/XOFF software flow control is correctly enabled, or switch to RTS/CTS hardware handshaking if the cabling permits. Always perform a hard reset on the control after modifying I/O parameters to ensure the new serial settings are initialized correctly by the Fagor communication firmware.
| Parameter | Value | Comments |
|---|---|---|
| In the control settings select 9 (Special Modes), 1 (General Parameters) | ||
| P000=5 | 2400 (Baud Rate) | |
| P001=1 | (8 Databits) | |
| P002=0 | (0=No Parity) | |
| P003=0 | (0=One Stop Bit) | |
| P004=0 | (Protocol) | |
| P005=NO | (PWONDNC) | |
| P006=NO | (DNCDEBUG) | |
| P007=0 | (AbortChr) | |
| P008=0 | (EolChr) | |
| P009=0 | (EofChr) | |
| P010=ON | (XonXoff) | |
| Reset Control After Making Changes. | ||
| In EasyDNC setting: Data Rate = 2400, 8 Databits, No Parity, 1 Stopbit, Flow Control = XonXoff, Mode=Auto | ||
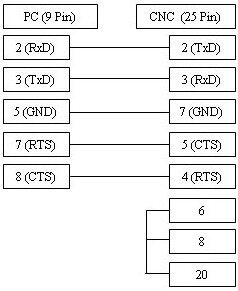
Cable Diagrams
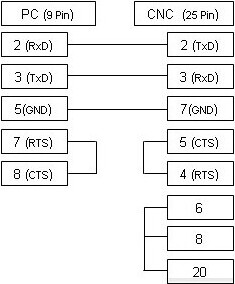
The cable diagram shown above is the most frequently used configuration and supports xOn/xOff (software) flow control (DC1/DC3). If your CNC machine is configured for RTS/CTS (hardware) flow control, please refer to the alternative connection diagram below.