Establishing reliable DNC communication for Mazak T32 and M2 controls requires precise configuration of parameters I1 through I58. Stable data transfer between your PC and CNC is critical for operational efficiency. When troubleshooting, prioritize verifying that your baud rate matches precisely across both the software and machine interfaces. Handshaking mismatches—often occurring between XON/XOFF (software) and RTS/CTS (hardware) protocols—are a frequent source of communication failure. While these controls may support 8-bit data configurations, we highly recommend 7 data bits with even parity to ensure robust, error-free serial transmission. Always confirm that stop bits and parity settings are strictly synchronized to avoid framing errors and transmission timeouts during DNC operation.
| Parameter | Value | Comments |
|---|---|---|
| I 1 | 2 | |
| I 2 | 3 | |
| I 3 | 0 | |
| I 4 | 0 | |
| I 5 | 3 | |
| I 6 | 3 | |
| I 7 | 1 | |
| I 8 | 5 | |
| I 9 | 0 | |
| I 10 | 1 | |
| I 11 | 1 | |
| I 12 | 0 | |
| I 13 | 0 | |
| I 14 | 0 | |
| I 15 | 30 | |
| I 16 | 0 | |
| I 24 | 0 | |
| I 58 | 0000 0000 | |
| Note: Although the Mazak may be set to 8 data bits with no parity, ensure that your DNC software is configured for 7 data bits with even parity for optimal performance. | ||
Cable Pinout
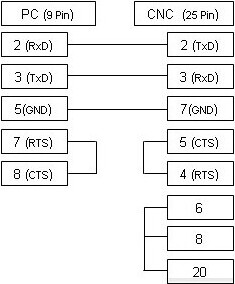
The cable illustrated above is the most commonly used configuration and supports xOn/xOff (DC1/DC3) flow control.
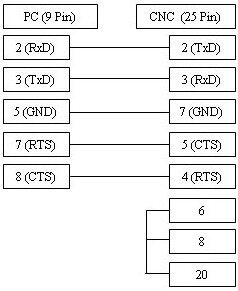
If your CNC machine is configured for RTS/CTS (hardware) flow control, please refer to the alternative wiring diagram above, which in most instances supports both communication handshaking methods.