The Mazak M32 control is a robust CNC system that enables efficient data transfer via DNC through precise parameter configuration. Establishing error-free serial communication (RS232) requires exact alignment of parameters G19 through G29. Pay close attention to baud rate and flow control settings to prevent data transmission errors during Mazatrol program transfers. This configuration guide assists you in setting up the appropriate pinout, whether you are utilizing XON/XOFF software handshaking or hardware-based RTS/CTS protocols. Successfully troubleshooting Mazak serial links often involves isolating common issues like baud rate mismatches or incorrect parity/stop bit alignment, which frequently cause buffer overflow or framing errors during data transmission. Always verify your cable shielding to reduce interference, and ensure that the port settings in your DNC software perfectly mirror the machine parameters to maintain stable and reliable machine-to-PC connectivity.
| Parameter |
Value |
Comments |
| G19 | 3 | 3 = 2400 Baud (5=600, 4=1200, 3=2400, 2=4800) |
| G20 | 3 | 2 stop bits |
| G22 | 0 | Even parity |
| G23 | 3 | 8 data bits (Set DNC software to 7) |
| G24 | 1 | - |
| G25 | 0 | - |
| G26 | 0 | - |
| G27 | 0 | Use ISO |
| G28 | 0 | - |
| G29 | 3 | - |
Note: Although the Mazak may be set to 8 data bits with no parity, ensure your DNC software is configured for 7 data bits with Even parity. Select XON/XOFF flow control within your DNC software.
Cable Wiring
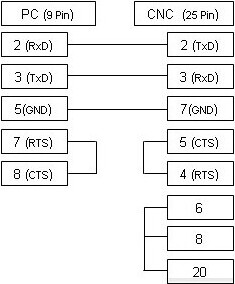
The cable illustrated above is the most commonly used version and supports XON/XOFF control (DC1/DC3).
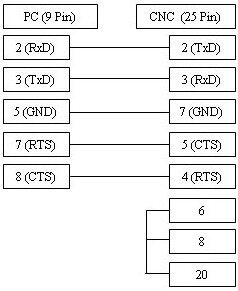
If your CNC machine is configured for RTS/CTS (hardware) flow control, use this alternative wiring diagram, which in most instances supports both types of flow control.