Mazak M Plus and T Plus controls require precise serial interface configuration to ensure reliable DNC data exchange. Correctly adjusting user parameters—specifically within group #5—is essential for maintaining a stable communication link between the CNC and your PC. A critical troubleshooting step involves the data bit setting: despite the control's internal 8-bit configuration, your DNC software must be set to 7 data bits to ensure seamless, error-free program transmission. Always verify that your baud rate matches precisely between devices to prevent framing errors, and ensure that your handshake protocol (XON/XOFF) is consistently applied on both ends to avoid buffer overflows during high-speed data transfer or complex tape-mode machining cycles.
| Parameter | Value | Comments |
|---|---|---|
| User Parameter #5 | ||
| G1 | 1 | Baud rate 9600 |
| G2 | 3 | 2 stop bits |
| G3 | 0 | Even parity |
| G5 | 3 | 8 data bits (Set software to 7) |
| G6 | 1 | - |
| G10 | 3 | xOn/xOff flow control (DC1/DC3) |
| G12 | 0 | No DC2/DC4 |
| G13 | 50 | - |
| G17 | 00000000 | - |
| G31 | 00000000 | - |
| G33 | 50 | - |
| G34 | 10 | - |
| G39 | 00000100 | - |
| G40 | 00000000 | - |
| G48 | 0 | - |
Note: Even though the Mazak is configured for 8 data bits, ensure your DNC software is set to 7 data bits. Select xOn/xOff flow control within your DNC software settings.
Cable Pinout
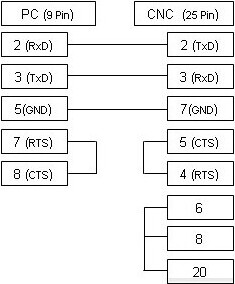
The cable on the left supports xOn/xOff (DC1/DC3) flow control.
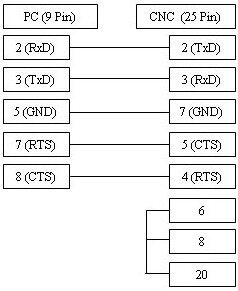
Use this alternative wiring diagram if RTS/CTS hardware flow control is required.