The Fanuc 12M and 12T controls are robust industry workhorses that require precise RS232 serial configuration for stable DNC communication. To ensure seamless data transfer between your PC and the CNC machine, verify that your baud rate, parity, and stop-bit parameters are precisely matched within EasyDNC. Communication timeouts or buffer overflows often stem from incorrect handshaking configurations; ensure your cable wiring aligns with the selected flow control mode (Software XON/XOFF vs. Hardware RTS/CTS). If data transfer fails, confirm your cabling follows the standard DTE/DCE pinouts to prevent signal polarity mismatches, which remain the most frequent cause of parity or framing errors in legacy Fanuc controller integration environments.
More information about the RS232-Port and the ALARM 086 (DR SIGNAL OFF / READER NOT READY) can be found here
More information about the ALARM 087 (Buffer Overflow) can be found here
| Parameter | Value | Comments |
|---|---|---|
| 5001 | 1 | |
| 5002 | 2 | |
| 5003 | 3 | |
| 5110 | 3 | |
| 5111 | 2 | |
| 5112 | 9 (Baud Rate) | |
| 5120 | 3 | |
| 5121 | 2 | |
| 5122 | 9 (Baud Rate) | |
| 5130 | 3 | |
| 5131 | 2 | |
| 5132 | 9 (Baud Rate) ** | |
| Drip Feed | Select TAPE mode on control, press Cycle Start, then SEND on PC. | |
| EasyDNC | Set Baud Rate, Parity, DataBits/StopBits as above. Mode: 'Auto or Fanuc'. | |
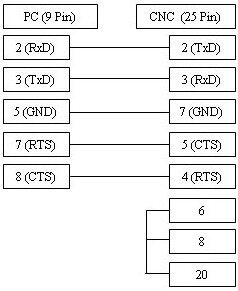
Cable Diagrams
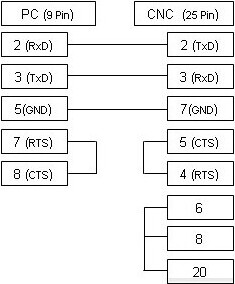
The cable illustrated above is the most commonly used version and supports xOn/xOff (DC1/DC3) flow control. If your CNC machine is configured for hardware RTS/CTS flow control, please refer to the alternative wiring diagram below.