Correctly configuring the serial interface for the Fanuc 21 control is essential for stable data transfer and DNC operation. Ensure precise synchronization of baud rate and I/O parameters to prevent common parity or framing errors. Reliable communication hinges on matching the control's handshake protocol—whether using XON/XOFF software flow control or RTS/CTS hardware handshaking—with your DNC software. Our guide assists you in setting up drip-feed (TAPE mode) connections, ensuring your programs are transmitted efficiently and securely. If you experience intermittent data loss, verify your cable shielding and ensure the baud rate is set consistently across both the CNC terminal and the host computer to maintain a stable bitstream.
| Parameter | Value | Comments |
|---|---|---|
| 0000 | 00000010 | |
| 0020 | 0 | |
| 0100 | 00100000 | |
| 0101 | 10000001 | |
| 0102 | 0 | |
| 0103 | 9 (BaudRate 2400) | |
| 6 = 300, 7 = 600, 8 = 1200, 9 = 2400, 10 = 4800, 11 = 9600 | ||
| TV Check | 0 = Disabled | |
| Punch Code | 1 = ISO | |
| Tape Format | 0 | |
| I/O Channel | 0 | |
| Drip Feed: Select TAPE mode on the control. Press Cycle Start. Then go to the computer, prepare the program and click 'Send'. | ||
| In EasyDNC set Baud Rate, Parity, DataBits and StopBits as above. Set 'Mode=Auto or Fanuc'. | ||
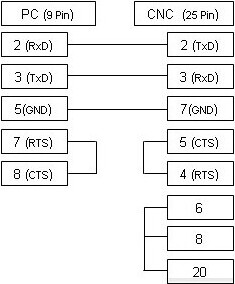
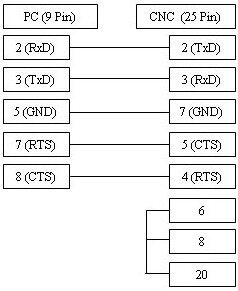
The cable shown above is the most commonly used variant and supports XON/XOFF (DC1/DC3) software flow control. If your CNC machine is configured for RTS/CTS (hardware) flow control, please refer to the alternative wiring diagram below, which in most cases supports both types of flow control.