Configuring the Fanuc 11 control (11M/11T) for DNC operations requires precise parameter matching to ensure stable serial data transfer. Establishing the correct baud rate, parity, and handshake protocol is critical for reliable NC program loading and seamless drip-feeding. Ensure your RS232 port settings are configured strictly in accordance with your hardware documentation to avoid parity errors, buffer overflows, or framing issues. When troubleshooting, verify that your handshake logic—whether software XON/XOFF or hardware RTS/CTS—is mirrored identically between the Fanuc control and your DNC software to prevent communication time-outs. Always perform a test transmission after updating parameters to confirm handshaking signals are correctly interpreted by the control unit.
| Parameter | Value | Comments |
|---|---|---|
| 5001 | 1 | |
| 5002 | 2 | |
| 5003 | 3 | |
| 5110 | 3 | |
| 5111 | 2 | |
| 5112 | 9 (Baud Rate) | |
| 5120 | 3 | |
| 5121 | 2 | |
| 5122 | 9 (Baud Rate) | |
| 5130 | 3 | |
| 5131 | 2 | |
| 5132 | 9 (Baud Rate) **
6 = 300 | 7 = 600 | 8 = 1200 | 9 = 2400 | 10 = 4800 | 11 = 9600 |
|
| TV On/Off | 0 = Disabled | |
| Punch Code | 0 = ISO | |
| Input device | 1 = 1 | |
| Input Device | 2 = 1 | |
| Drip Feed: Select TAPE mode on the controller and press Cycle Start. Then, transmit the file from the computer. In EasyDNC: Set Baud Rate, Parity, DataBits, and StopBits as shown above. Set 'Mode' to 'Auto' or 'Fanuc'. | ||
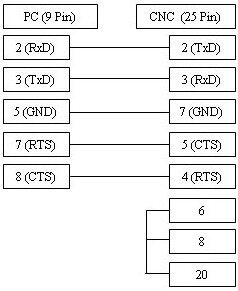
Cable Connection
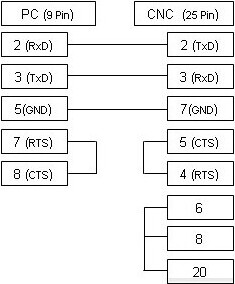
The cable shown above is the most frequently used configuration and supports XON/XOFF flow control (DC1/DC3). If your CNC machine is configured for RTS/CTS (hardware) flow control, please refer to the alternative wiring diagram provided below.