Fanuc 15M and 15T controls are high-performance industrial controllers engineered for precision CNC milling and turning applications. To ensure seamless data transfer and DNC communication, precise configuration of RS232 serial parameters is mandatory. Misalignment in baud rate, parity, or flow control settings between the machine control and your DNC software is the leading cause of communication timeouts and framing errors. Always verify that your stop bits and flow control (Software XON/XOFF vs. Hardware RTS/CTS) match the cable wiring configuration to prevent data loss or buffer overflow during high-speed drip-feeding operations. Ensuring these settings are synchronized will provide stable, reliable performance on the shop floor.
More information about the RS232-Port and the ALARM 086 (DR SIGNAL OFF / READER NOT READY) can be found here
More information about the ALARM 087 (Buffer Overflow) can be found here
| Parameter | Value | Comments |
|---|---|---|
| 5001 | 1 | |
| 5002 | 2 | |
| 5003 | 3 | |
| 5110 | 4 | |
| 5111 | 2 | |
| 5112 | 9 (Baud Rate) | |
| 5120 | 4 | |
| 5121 | 2 | |
| 5122 | 9 (Baud Rate) | |
| 5130 | 4 | |
| 5131 | 2 | |
| 5132 | 9 (Baud Rate) ** | |
| 6=300, 7=600, 8=1200, 9=2400, 10=4800, 11=9600 | Baud Rate Selection | |
| TV On/Off | 0 = Disabled | |
| Punch Code | 0 = ISO | |
| Input device | 1 | |
| Output Device | 1 | |
| Drip Feed: Select TAPE mode, press cycle start, then send from computer. | ||
| EasyDNC Setup: Baud Rate as above, Databits/Parity 7, Even, Stopbits 2. Set 'Mode=Auto or Fanuc'. | ||
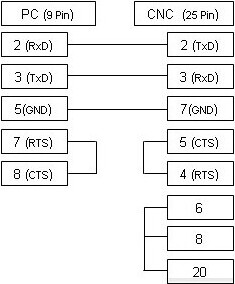
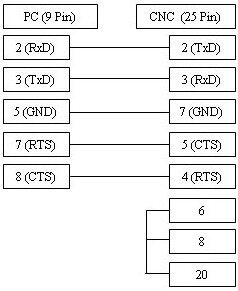
The cable illustrated above is the most commonly used configuration and supports xOn/xOff (software) flow control (DC1/DC3). If your CNC machine is configured for RTS/CTS (hardware) flow control, please refer to the alternative wiring diagram below, which is designed to support both methods of flow control in most industrial applications.