The Fanuc OM control is a standard-bearer in precision machining, requiring exact serial interface parameters for stable DNC operation. Proper configuration of communication settings—including baud rate, parity, and stop bits—is critical to preventing buffer overflows and transmission errors during Drip-Feed execution. Always ensure that the I/O channel on the control matches your port settings to maintain a reliable handshake. Common pitfalls include mismatched handshaking protocols (XON/XOFF vs. RTS/CTS) and incorrect stop bit settings, which can cause intermittent data loss or "alarm" triggers on the machine side. Verify your cable shielding and ground integrity, as noise interference in industrial environments is a frequent cause of DNC communication failures when utilizing standard RS-232 serial interfaces for Fanuc controls.
More information about the RS232-Port and the ALARM 086 (DR SIGNAL OFF / READER NOT READY) can be found here
More information about the ALARM 085 (Parity/Communications Error) can be found here
More information about the ALARM 087 (Buffer Overflow) can be found here
| Parameter | Value | Comments |
|---|---|---|
| 0002 | 0000 0001 | |
| 0552 | 9 (Baud Rate) | |
| 6 = 300, 7 = 600, 8 = 1200, 9 = 2400, 10 = 4800, 11 = 9600 | ||
| TV On/Off | 0 = Disabled | |
| Punch Code | 1 = ISO | |
| I/O Channel | 0 | |
| Drip Feed: Enable Para G127.5. Select Auto/DNC Mode on the control. Press Cycle Start. Then go to the computer, prepare the program and click 'Send'. | ||
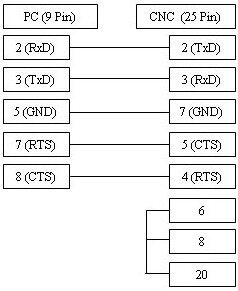
Cable Diagrams and Notes
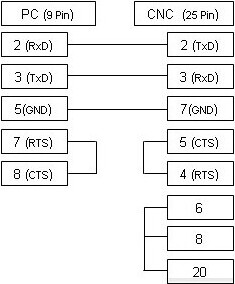
The cable illustrated above is the most commonly used configuration and supports xOn/xOff (Software) flow control (DC1/DC3). If your CNC machine is configured for RTS/CTS (Hardware) flow control, please refer to the alternative wiring diagram provided below.