The Fanuc 18 control, available in both M (milling) and T (turning) configurations, remains a robust industrial benchmark. Achieving reliable data transfer and DNC (drip-feed) operations requires precise RS232 interface configuration. To prevent common transmission errors, ensure exact matching of baud rates and I/O channel settings within parameters 0000 through 0103. Troubleshooting often reveals that communication failures stem from handshake mismatches; specifically, confirm whether your setup requires software (XON/XOFF) or hardware (RTS/CTS) flow control. Discrepancies here often manifest as buffer overflows or partial program truncation. Verify that parity, stop bits, and baud rates are synchronized between the DNC software and the machine control to eliminate framing errors and ensure consistent, high-speed data transmission for complex machining cycles.
More information about the RS232-Port and the ALARM 086 (DR SIGNAL OFF / READER NOT READY) can be found here
| Parameter | Value | Comments |
|---|---|---|
| 0000 | 00000010 | |
| 0020 | 0 | |
| 0100 | 00100000 | |
| 0101 | 10000001 | |
| 0102 | 0 | |
| 0103 | 9 (BaudRate 2400) | |
| 6 = 300, 7 = 600, 8 = 1200, 9 = 2400, 10 = 4800, 11 = 9600 | ||
| TV Check | 0 = Disabled | |
| Punch Code | 1 = ISO | |
| I/O Channel | 0 | |
| Drip Feed: Set the control to TAPE mode. Press Cycle Start. Prepare the program on the computer and click 'Send'. | ||
| In EasyDNC, configure the Baud Rate, Parity, Data Bits, and Stop Bits to match the values above. Set the Mode to 'Auto' or 'Fanuc'. | ||
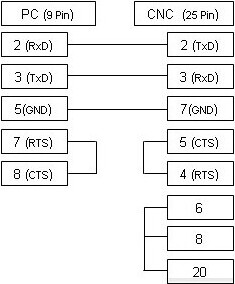
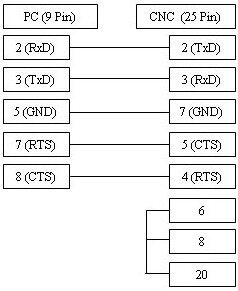
The cable illustrated above is the most common variant and supports xOn/xOff (DC1/DC3) flow control. If your CNC machine is configured for RTS/CTS (hardware) flow control, please refer to the alternative connection diagram below, which typically supports both types of flow control in most applications.