Establishing reliable DNC communication for the Fanuc OP control requires precise parameter configuration to ensure seamless data exchange between your workstation and the CNC machine. Proper alignment of baud rate, parity, and stop bits is critical to prevent transmission errors and buffer overflows. Ensure that both the machine-side parameters and your DNC software settings (e.g., EasyDNC) match exactly to facilitate efficient NC program transfer. If you encounter checksum or parity errors, verify that your software flow control matches the hardware jumper configuration; misaligned handshaking between software XON/XOFF and hardware RTS/CTS is a frequent cause of intermittent data loss during long program uploads.
| Parameter | Value | Comments |
|---|---|---|
| 340 | 2 | |
| 341 | 2 | |
| 311 | 0011 1000 (Baud 2400) | |
| - | 0011 0110 = 600 | |
| - | 0011 0111 = 1200 | |
| - | 0011 1000 = 2400 ** | |
| - | 0011 1001 = 4800 | |
| - | 0011 1010 = 9600 | |
| TV On/Off | 0 = Disabled | |
| Punch Code | 1 = ISO | |
| Input device | 1 = 1 | |
| Input Device | 2 = 1 | |
| In EasyDNC set Baud Rate, Parity, DataBits and StopBits as above. Set 'Mode=Auto or Fanuc' | ||
Cable Connection and Hardware
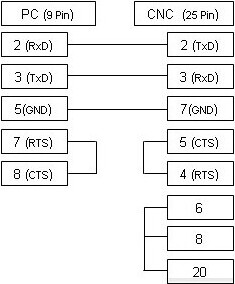
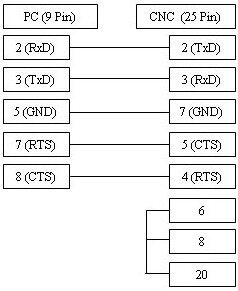
The cable configuration shown above is the most common implementation, supporting xOn/xOff (software) flow control (DC1/DC3). If your CNC machine is specifically configured for RTS/CTS (hardware) flow control, please refer to the alternative wiring diagram below. In many instances, the diagram below will support both methods of flow control depending on the specific machine implementation.