Establishing reliable DNC communication for the Fanuc 10 control requires precise serial interface parameterization. Successful drip-feeding (TAPE mode) is contingent upon perfectly matched baud rate, parity, and handshaking protocols (XON/XOFF or hardware flow control). To prevent buffer overflows or transmission data loss, ensure that your PC-side EasyDNC settings exactly mirror the CNC's internal machine parameters. Common pitfalls include mismatched stop bits or cable pinout inconsistencies; verify that your cables are shielded and that the flow control method selected in the software aligns with the machine's I/O configuration. Consistent adherence to these standards ensures stable, error-free program execution during high-speed machining operations.
More information about the RS232-Port and the ALARM 086 (DR SIGNAL OFF / READER NOT READY) can be found here
More information about the ALARM 087 (Buffer Overflow) can be found here
More information about the ALARM 085 (Parity/Communications Error) can be found here
| Parameter | Value | Comments |
|---|---|---|
| 5001 | 1 | |
| 5002 | 2 | |
| 5003 | 3 | |
| 5110 | 3 | |
| 5111 | 2 | |
| 5112 | 9 (Baud Rate) | |
| 5120 | 3 | |
| 5121 | 2 | |
| 5122 | 9 (Baud Rate) | |
| 5130 | 3 | |
| 5131 | 2 | |
| 5132 | 9 (Baud Rate) ** | |
| 6 = 300 | 7 = 600 | |
| 8 = 1200 | 9 = 2400 ** | |
| 10 = 4800 | 11 = 9600 | |
| TV On/Off | 0 = Disabled | |
| Punch Code | 0 = ISO | |
| Input device | 1 = 1 | |
| Input Device | 2 = 1 | |
| Drip Feed: Select TAPE mode on the controller and press Cycle Start. Then, trigger the transmission from your PC. | ||
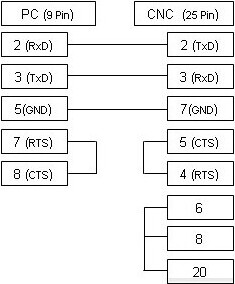
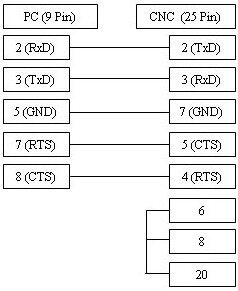
The cable illustrated above is the most frequently utilized configuration, supporting xOn/xOff (software) flow control (DC1/DC3). If your CNC machine is specifically configured for RTS/CTS (hardware) flow control, please refer to the alternative connection diagram provided below, which is generally compatible with both handshaking methods.