Correct RS232 interface configuration for Hinumerik 3000M and 3000T controllers is vital for reliable DNC operation. By adjusting machine parameters 411, 412, and 416, you synchronize baud rates and communication protocols between the CNC and your PC. We strongly recommend using RTS/CTS hardware handshaking for maximum stability, though XON/XOFF software flow control remains a viable fallback for legacy serial environments. Common troubleshooting includes verifying baud rate parity, ensuring matching stop bits, and resolving handshake mismatches. If data transmission errors occur, re-verify that the DTE/DCE pinouts are properly mapped for the cable length, as signal attenuation can often lead to parity errors or buffer overflows in older serial hardware configurations.
| Parameter | Value | Comments |
|---|---|---|
| 411 | 1110 1101 | = 2400 Baud. (1110 1011 = 600, 1110 1100 = 1200, 1110 1110 = 4800) |
| 412 | 1110 1101 | = 2400 Baud. (1110 1011 = 600, 1110 1100 = 1200, 1110 1110 = 4800) |
| 416 | 1xxxxxx1 | x = Leave unchanged |
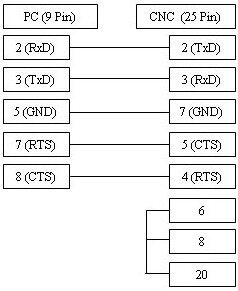
Cable Pinout and Notes
Select RTS/CTS flow control within your DNC software. The cable layout shown here is compatible with both XON/XOFF (DC1/DC3) and RTS/CTS handshaking, ensuring reliable operation in most production environments.
For simplified setups without hardware handshaking, a 3-wire cable configuration can be utilized. A wiring diagram for this application can be found here.
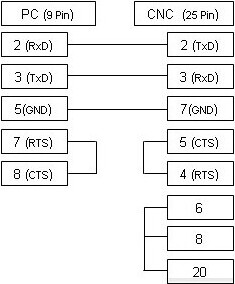
RS232 Cable: 9-pin (PC) to 25-pin (CNC)