Configuring the RS232 serial interface on Hinumerik 2000M and 2000T controls requires precise adjustment of machine parameters. Establishing stable data transmission between your PC and CNC relies on matching baud rates and handshake protocols, such as RTS/CTS or XON/XOFF. Incorrect settings frequently lead to framing errors or buffer overflows during DNC cycles. Our configuration guide helps you troubleshoot common communication pitfalls, including parity mismatches and stop bit inconsistencies, ensuring robust performance. By correctly syncing your DNC software with the machine’s hardware-level communication requirements, you minimize production downtime and maintain signal integrity throughout your manufacturing process. This setup procedure is optimized for reliable serial connectivity in modern workshop environments.
| Parameter | Value | Comments |
|---|---|---|
| 5010 | 0 | (00000000) |
| 5012 | 0 | (00000000) |
| 5011 | 11000101 | = 2400 Baud. For other baud rates see table below |
| 5013 | 11000101 | = 2400 Baud. For other baud rates see table below |
| 11000011 = 600 | 11000100 = 1200 | 11000101 = 2400 | 11000110 = 4800 | ||
| 5016 | xx10xxxx | x = Leave unchanged |
| RTS | Line 1 | Select RTS/CTS handshaking in the DNC software. |
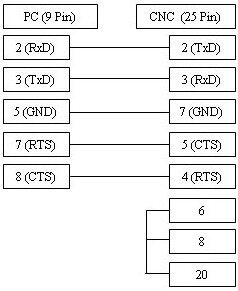
Cable Pinout and Notes
The cable illustrated supports both XON/XOFF (DC1/DC3) and RTS/CTS (hardware flow control). If you intend to use strictly XON/XOFF transmission, a simplified 3-wire cable configuration is also viable. A corresponding diagram can be found here.
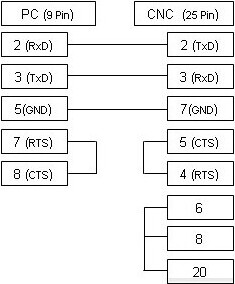
RS232 Cable: 9-pin (Computer) to 25-pin (CNC)