The Heidenhain TNC 155 control remains a reliable workhorse in modern machine shops. Establishing stable DNC communication between your PC and CNC requires precise Machine Parameter (MP) configuration and proper physical cabling. Troubleshooting common serial issues, such as baud rate mismatches or data parity errors, is critical for seamless NC program transfers. Ensure your handshaking protocols—whether utilizing XON/XOFF software flow control or hardware RTS/CTS—are matched perfectly between the control and your DNC software. Properly configured cabling will eliminate character loss and transmission timeouts, significantly boosting your production floor efficiency and workflow reliability.
| Parameter | Value | Comments |
|---|---|---|
| MP232 | 0 | |
| MP71 | 515 | |
| MP222 | 104 | |
| In DNC software: Baud rate 2400, 7 data bits, even parity, 2 stop bits. | ||
| Select RTS/CTS flow control in the DNC software. The software should insert STX (02) and ETX (03) codes. |
Cable Diagrams and Notes
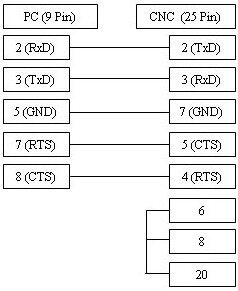
The cable illustrated below supports both XON/XOFF (DC1/DC3) and RTS/CTS (hardware flow control) and is suitable for most TNC 155 installations.
For a simpler 3-wire connection (XON/XOFF only or no flow control), use the diagram found here.
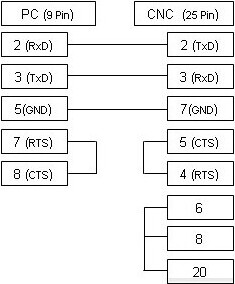
RS232 Cable: 9-pin computer to 25-pin CNC