The Heidenhain TNC 355 is a robust, precision-oriented CNC control widely respected for high-accuracy milling operations. Establishing reliable DNC communication between your workstation and the control requires precise configuration of Machine Parameters (MP) and verified RS232 serial cabling. To prevent data corruption or buffer overflows during program transmission, ensure the baud rate, parity, and stop bit settings are perfectly synchronized between the software and the control. Common pitfalls include mismatched handshake protocols—such as confusion between hardware (RTS/CTS) and software (XON/XOFF) flow control—and incorrect cable shielding. Following these standardized settings will ensure seamless NC program handling and reduce transmission errors common in older serial environments.
| Parameter | Value | Comments |
|---|---|---|
| MP232 | 0 | |
| MP71 | 515 | |
| MP222 | 104 | |
| In the DNC software set: Baud rate 2400, 7 Data Bits, Even Parity, 2 Stop Bits. | ||
| Select RTS/CTS flow control in your DNC software. The DNC software must append STX and ETX codes to the transmission. ASCII Start Code = STX (02), ASCII End Code = ETX (03). |
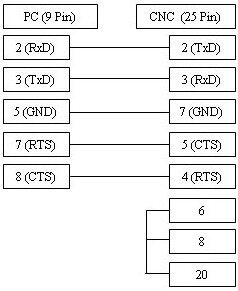
The cable configuration shown below supports both XON/XOFF (DC1/DC3) and RTS/CTS (hardware flow control), making it the recommended standard for most installations.
If you are certain your CNC does not require hardware handshaking—or explicitly requires only XON/XOFF—a simplified 3-wire cable may be used. See the diagram here.
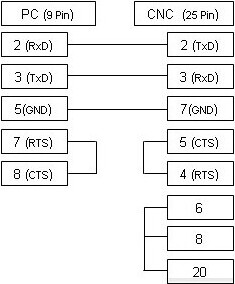
RS232 Cable.
9-pin computer to 25-pin CNC