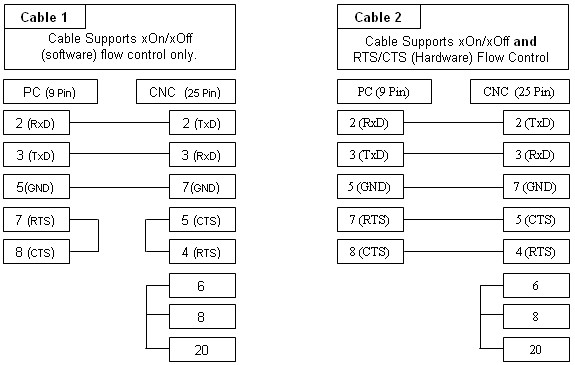
The Siemens Sinumerik 810M and 810T controls are robust industrial systems requiring precise DNC parameter configuration to ensure error-free data transmission. To establish a reliable serial link, verify that baud rate, parity, and stop bit settings match precisely between your DNC software and the machine controller. Common communication failures often stem from handshake mismatches; ensure your RTS/CTS hardware flow control or XON/XOFF software flow control is configured to mirror the controller's I/O requirements. Using shielded, high-quality RS232 cabling is essential to prevent signal degradation and parity errors during high-speed data transfers. Always validate your cable pinout against the Siemens standard to avoid ground loops or signal floating, which frequently disrupt extended DNC drip-feed operations in shop-floor environments.
| Parameter | Value | Comments |
|---|---|---|
| 5010 | 0 | |
| 5012 | 0 | |
| 5011 | 1111 0101 | = Baud rate 2400 |
| 5013 | 1111 0101 | See Baud Rate Table |
| 1111 0011 = 600 | 1111 0100 = 1200 | 1111 0101 = 2400 | 1111 0110 = 4800 | ||
| RTS-Line | 1 | |
Cable Type 1 is widely used, but Cable 2 is recommended as it supports both software and hardware flow control, offering greater compatibility across various CNC types and operating modes.