The Heidenhain TNC 145 remains a cornerstone of precision machining, known for its industrial reliability. To optimize your CNC workflow and ensure seamless DNC data transmission between the machine tool and your PC, configuring the RS232 serial interface correctly is critical. By accurately setting parameters such as baud rate, parity, and flow control, you can eliminate communication errors and boost shop-floor productivity.
| Parameter | Value | Comments |
|---|---|---|
| Baud rate | 2400 | - |
| Parity | Even | - |
| Data bits | 7 | - |
| Stop bits | 2 | - |
|
Select RTS/CTS flow control within your DNC software. The software should be configured to include STX and ETX codes during data transmission. ASCII Start Code = STX (02), ASCII End Code = ETX (03). |
||
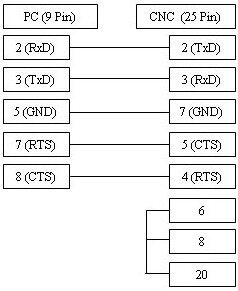
The illustrated cable is compatible with both xOn/xOff (DC1/DC3) and RTS/CTS (Hardware flow control). For basic configurations where hardware flow control is not supported, a simple 3-wire cable may be used. View the diagram here.
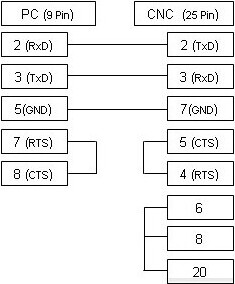
RS232 Cable: 9-pin PC to 25-pin CNC