Configuring Fanuc 6M and 6T controllers requires precise adjustment of parameters 340 and 341, alongside parameter 311 for baud rate synchronization. As a legacy CNC control system, the Fanuc 6 series utilizes a robust serial interface. By establishing correct parameters and using a properly pinned RS232 cable, you ensure reliable data flow for your DNC system. When setting up, pay close attention to the selection of ISO code and the appropriate flow control (XON/XOFF vs. hardware RTS/CTS) to prevent communication time-outs or buffer overflow errors. Ensure that the parity and stop bits defined in your DNC software strictly mirror the CNC controller’s internal registers to maintain data integrity and avoid "LSK" or "Buffer" alarm signals during long-program drip-feeding or machine-side memory loading.
| Parameter | Value | Comments |
|---|---|---|
| 340 | 2 | |
| 341 | 2 | |
| 311 | 0001 1000 (Baud 2400) | |
| 0001 0110 = 600 | ||
| 0001 0111 = 1200 | ||
| 0001 1000 = 2400 ** | ||
| 0001 1001 = 4800 | ||
| 0001 1010 = 9600 | ||
| TV On/Off | 0 = Disabled | |
| Punch Code | 1 = ISO | |
| Input Unit | 0 | |
| Input device | 1 = 1 | |
| Input Device | 2 = 1 | |
| In EasyDNC set Baud Rate, Parity, DataBits and StopBits as above. Set 'Mode=Auto or Fanuc' | ||
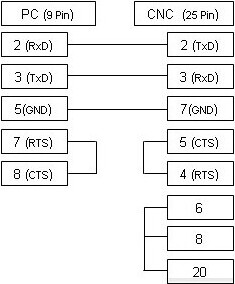
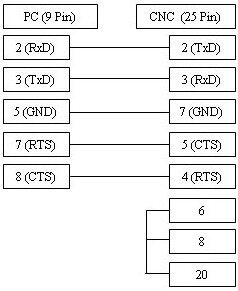
The cable illustrated above is the most frequently used version and supports XON/XOFF flow control (DC1/DC3). If your CNC machine is configured for RTS/CTS (hardware) flow control, please refer to the alternative connection diagram below, which in most cases supports both types of flow control.